Since the early 1980s there has been much discussion regarding various approaches and methods in the use of environmental stress screening and HALT/HASS to markedly improve product quality and life. Unfortunately, there was widespread misunderstanding and misapplication of the methodology, and some still remains. Accordingly, we have listed the "Seven Deadly Sins of HALT/HASS".
| Sin | What goes wrong | Do this instead |
|---|---|---|
| 1. Cycling chamber air instead of product | The product never expands and contracts fast enough | Stimulate the product thermally, at a high rate of change |
| 2. Measuring vibration on the table | The input is measured, not the product's response | Measure the product's response to 6-DoF vibration |
| 3. Putting latent defects into product | HASS overstress creates new defects | Find the optimum stress levels empirically |
| 4. Taking out too much product life | The screen is set too high | Keep the screen no higher than it needs to be |
| 5. Not tailoring HASS to the product | One screen is too low for some products, too high for others | Tailor the screen to each product |
| 6. Not functionally testing during HALT/HASS | Intermittent failures go undetected | Power and test the product throughout |
| 7. Over-designing after an improper HALT | Undue overstress drives needless redesign | Fix real weak parts; avoid redesign for undue overstress |
1. Thermal cycling chamber air instead of product
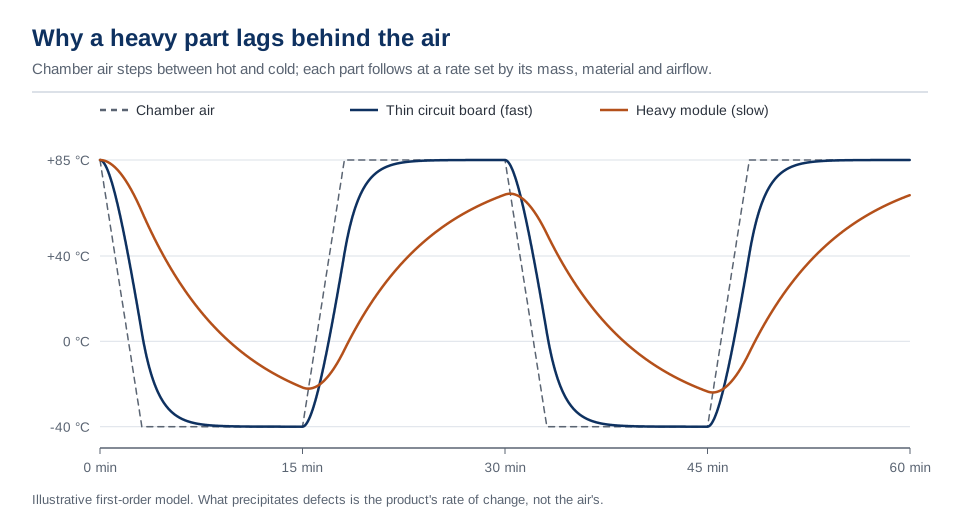
Environmental chambers with high rates of air temperature change may not qualify as a HALT/HASS chamber. Simply cycling chamber air temperature is not sufficient. HALT/HASS requires thermal stimulation of the product.
Thermal cycling must cause the product to physically expand and contract at a relatively high rate of change over a number of stress cycles. That is why you cannot simply use traditional environmental simulation chambers or sell them with a "HALT/HASS" label.
2. Vibration levels measured on table instead of product
As in product thermal stimulation, HALT/HASS requires a product vibration response. Measurement of the input is not measurement of the product response to 6-DoF vibration.
3. Putting latent defects into product
HASS overstress, whether thermal, vibration, humidity or other, can cause new latent defects, which were not there to begin with.
Each product is different. It is vitally important to determine the optimum stress levels empirically when establishing a HASS production screen.
4. Taking out too much product life
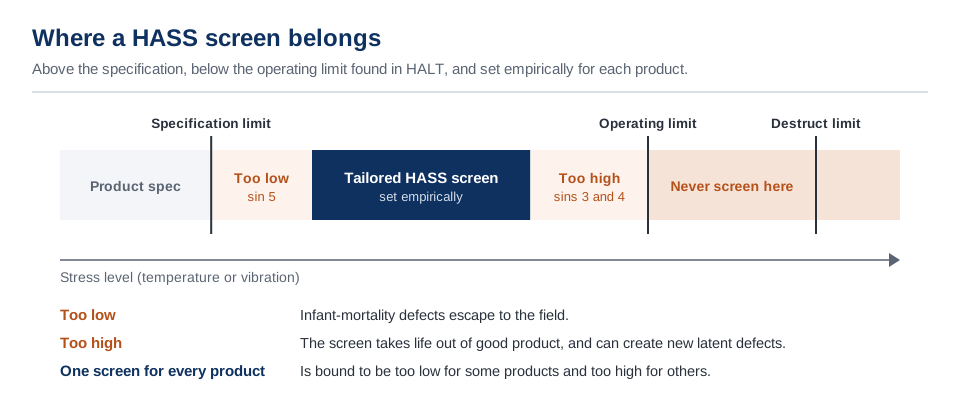
HASS screening during manufacturing can take unneeded life out of a product if the screen is set too high or a one-screen-fits-all approach is used.
5. Not tailoring HASS stress to product
It is imperative that the HASS screens be tailored to the product. The one-screen-fits-all approach does not work. The screen level may be too low or too high for some products. If too low it can allow potential infant mortality defects to be undetected. If too high it can take unneeded life out of the product.
6. Not functionally testing product while undergoing HALT/HASS
Intermittent part failures can go undetected unless they are functionally tested while undergoing HALT/HASS. The level of detectability must be high in order to obtain the results desired.
7. Over-design of product as a result of improper HALT
HALT is essentially an exploratory stress test to find part defects and to replace weak parts with robust parts. However, care must be taken that the product is not subjected to HALT undue overstress and consequential redesign. Misapplication of HALT can result in an over-designed product that is not commercially viable.
We can help
Our long-term experience with HALT/HASS seminars, installations, and practitioners worldwide is a valuable resource that we welcome you to draw on. Please do not hesitate to contact us.