ESS, HALT and HASS are three applications of one idea: apply environmental stress to a product on purpose, so defects show up in your lab instead of at a customer site. Environmental Stress Screening (ESS) is the umbrella method. HALT — Highly Accelerated Life Testing — applies it during development to find a design's limits. HASS — Highly Accelerated Stress Screening — applies it on the production line to catch units built with a defect.
The short answer
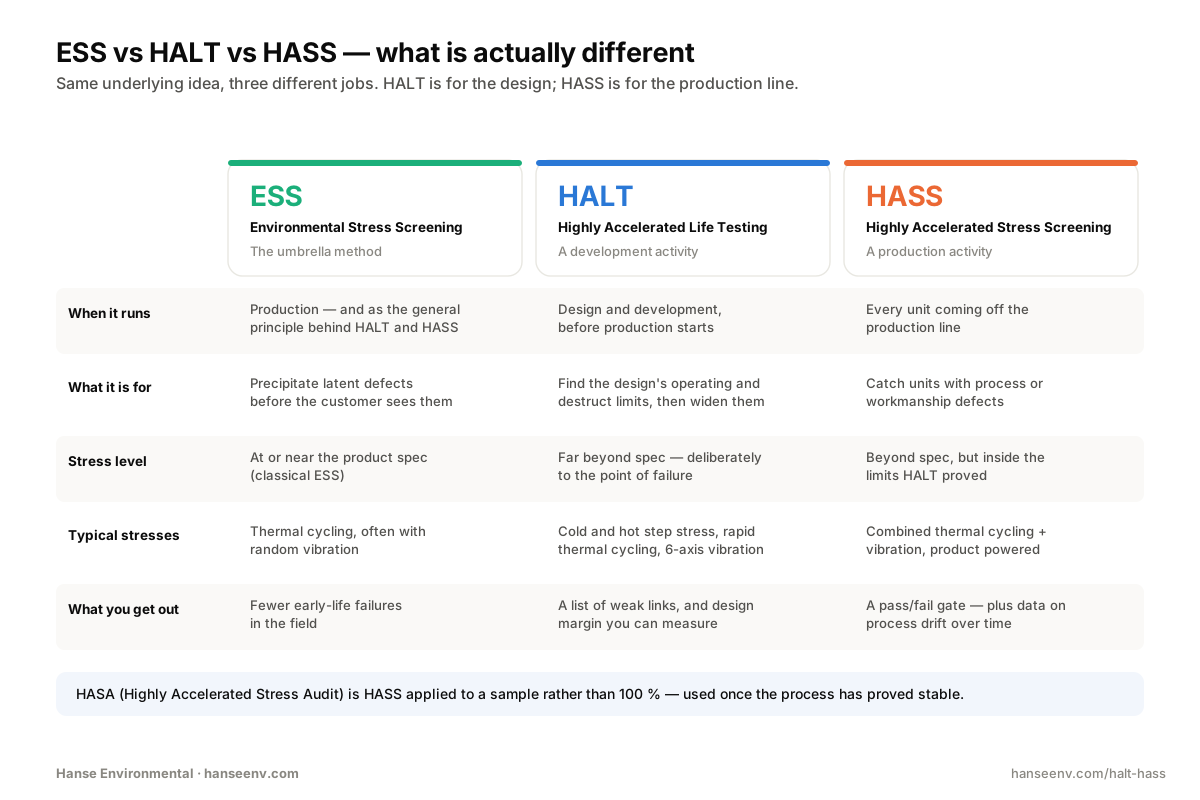
- ESS (Environmental Stress Screening) — thermal cycling, usually combined with vibration, applied to finished product to precipitate latent defects before shipment.
- HALT (Highly Accelerated Life Testing) — a development test that steps stress well past the specification until the unit stops working and then until it breaks, so weak links can be designed out.
- HASS (Highly Accelerated Stress Screening) — a production screen that uses stress levels derived from HALT results, applied to every unit, with the product powered and functionally tested while it is being stressed.
The distinction that matters most: HALT tests a design. HASS tests a build. You cannot run a sensible HASS screen until HALT has told you where the edges are.
Why good products still fail early
Product life cycles are short and getting shorter. A new model of almost anything — a controller, a power supply, a medical instrument — is expected within months, and customers expect it to work out of the box, every time.
That pressure compresses development and manufacturing. What gets squeezed out shows up later as part defects, process defects and workmanship defects: a marginal solder joint, a connector that is seated but not fully latched, a component running closer to its rating than anyone realized. These are latent defects — real, but not yet detectable, because under benign bench conditions the unit works fine.
A latent defect eventually becomes a patent (detectable) failure once enough thermal cycling, mechanical fatigue or time has been applied. The question is only where that happens: in your factory, or in your customer's plant.
The classic way to picture this is the bathtub curve.
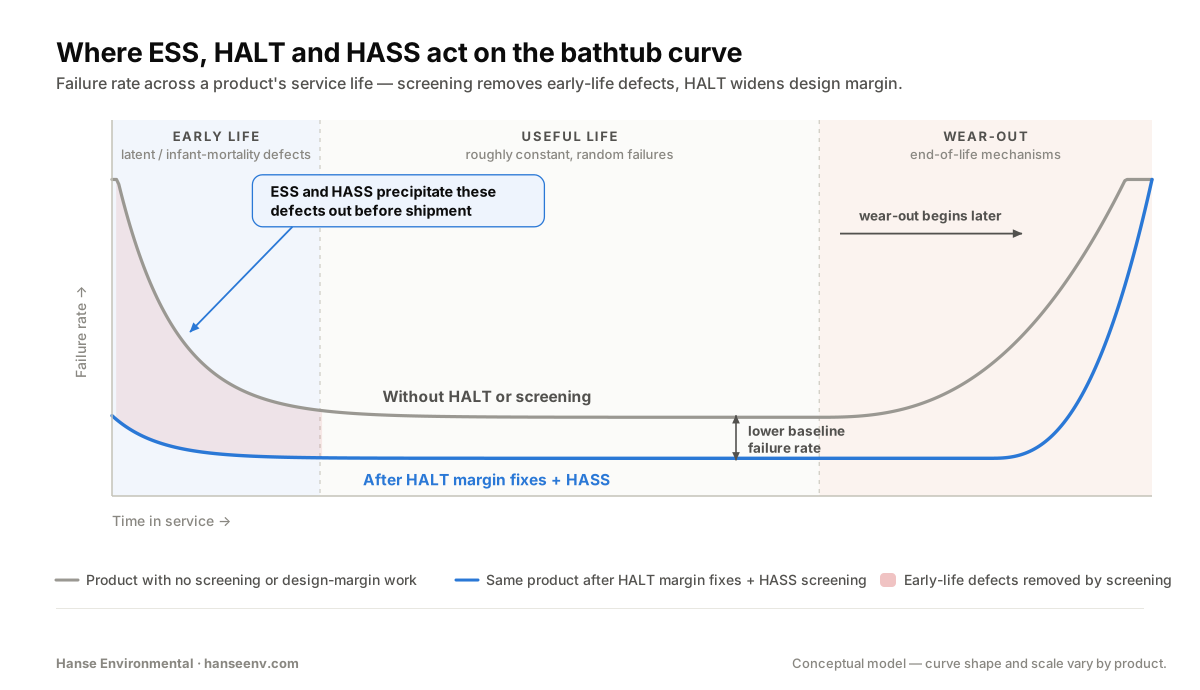
The early-life region is what screening exists to remove. The height of the flat middle section, and how soon the wear-out tail starts to climb, are what design margin work — HALT — is meant to improve.
What is Environmental Stress Screening (ESS)?
Environmental Stress Screening is the practice of applying environmental stress — most commonly rapid thermal cycling, often with random vibration — to manufactured product in order to precipitate latent defects before the product ships.
How ESS works
Thermal cycling works because the materials inside an assembly expand and contract at different rates. A ceramic capacitor, its solder joint, the copper pad and the FR-4 laminate underneath all move by different amounts for the same temperature change. Cycle that repeatedly and quickly, and a marginal joint accumulates strain until it opens.
Vibration works on a different mechanism — fatigue in leads, wires, fasteners and connectors, plus relative motion between parts that should not be moving relative to each other. Because the two mechanisms find different defects, ESS is far more effective with both than with either alone.
The stress has to reach the parts, not just the air around them. That is why product change rate* matters more than the chamber's advertised air change rate, and why ESS chambers are built for rapid transitions rather than for tight steady-state control.
Classical ESS profiles and where they came from
Early ESS practice was codified in defense documents, and those profiles are still a reasonable starting point when you have nothing else. The best known is NAVMAT P-9492, the Navy manufacturing screening program:
| Parameter | NAVMAT P-9492 guidance |
|---|---|
| Random vibration | 6.0 GRMS overall, 20–2000 Hz, 0.04 g²/Hz plateau |
| Vibration duration | 10 minutes single axis, or 5 minutes in each of three orthogonal axes |
| Temperature range | −65 °F to 131 °F (approx. −54 °C to +55 °C), or at least a 160 °F span |
| Rate of change | 1 °F to 40 °F per minute, measured on the internal parts |
| Dwell | Until internal parts are within 5 °F of the set point |
| Cycles | 1 cycle (simple assembly) up to 10 cycles (very complex), last cycle failure-free |
MIL-STD-2164 covered the ESS process itself; it was canceled in 1996 and superseded by the handbook MIL-HDBK-2164A, which was itself made inactive in March 2025. Sector standards also exist — IPC-9592B makes HALT a requirement for power conversion devices in computing and telecom, and treats HASS as a route to reducing burn-in time. Which standards call for HALT and HASS, and which are qualification tests, is set out in our HALT/HASS standards guide.
Where classical ESS falls short
A fixed profile taken from a document was never tailored to your product. It may be far too gentle to precipitate anything in a rugged assembly, and it may be dangerously close to the limits of a delicate one. Classical ESS also generally runs at or near specification levels, which is exactly where a latent defect is least likely to reveal itself.
HALT and HASS were developed to close that gap: rather than borrowing someone else's numbers, you measure your own product's limits first, then screen inside them.
What is HALT (Highly Accelerated Life Testing)?
HALT is a development test. Temperature, vibration and the two combined are stepped well past the specification until the unit stops working and then until it is damaged, to find its operating and destruct limits and the weak links behind them; the weaknesses are then designed out, and the margin between the limits and the field environment is what the program delivers. HALT is not a pass/fail qualification test, and it does not predict MTBF or service life.
Full answer: What is HALT testing?
What is HASS (Highly Accelerated Stress Screening)?
HASS puts what HALT learned to work in production. Every unit runs a short combined thermal and vibration screen, above the product specification but below the operating limits HALT established, so the product can be powered and monitored throughout: a precipitation screen turns latent defects into detectable failures, and a detection screen catches them. The screen is proven safe and effective before it is used (Proof of Screen), and once the process is stable it can move to sampling (HASA).
Full answer: What is HASS testing?
How it all fits together
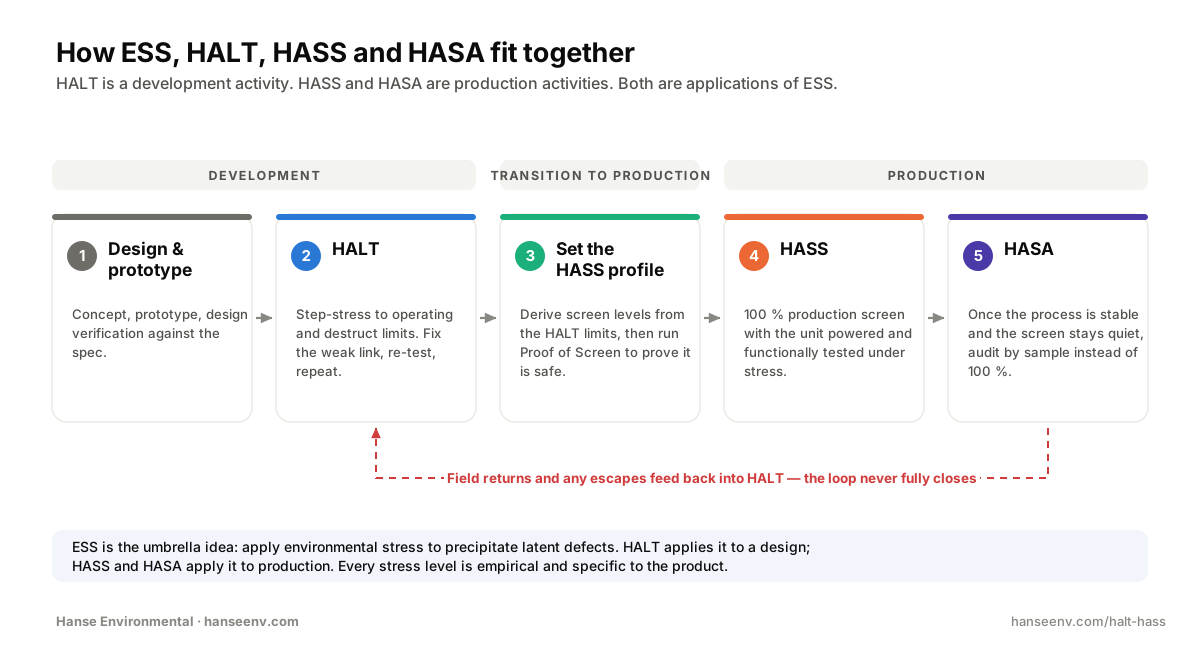
What the equipment actually has to do
Running HALT and HASS properly is not something a conventional temperature chamber can do. The requirements are specific:
- Very high product change rates*. Ramp rates measured on the product, not just on the return air. Most systems that achieve this use liquid nitrogen cooling with high-capacity heating; mechanically refrigerated non-nitrogen HALT systems exist, generally with lower ramp capability.
- A wide temperature range — roughly −100 °C to +200 °C, so you can pass the destruct limits of most electronics.
- Six-degree-of-freedom repetitive shock vibration, broadband rather than single-axis sine, so that resonances anywhere in the assembly get excited.
- Functional test access — cable feedthroughs, ports, and enough room to keep the unit powered and instrumented while the profile runs.
- Programmable, repeatable profiles, because a screen that is not repeatable is not a screen.
Hanse Environmental builds this equipment. The VTC line of HALT/HASS chambers runs from a 12 × 12 in (305 × 305 mm) table (VTC-1) up to 70 × 70 in (1,778 × 1,778 mm; VTC-36), with a 48 × 102 in (1,219 × 2,591 mm) VTC-32 for long assemblies. Across the line: 6-DoF tri-axial vibration spanning 10 Hz to 10,000 Hz with roughly 90% of the energy between 10 and 4,000 Hz. From the VTC-4 up: a −100 °C to +200 °C range, a 70 °C/min* temperature change rate over −65 to +100 °C, and up to 100 GRMS. The VTC-1 and VTC-1.5 run −75 °C to +175 °C and 70 GRMS as standard, with −100/+200 °C and 100 GRMS available as options, and the VTC-1 is 50 °C/min standard. The whole line uses liquid nitrogen direct injection, and heating, LN2 cooling and vibration are all driven with variable, proportional output rather than on/off switching (proportional LN2 control is standard on the VTC-4 and up), which cuts LN2 consumption substantially versus conventional on/off valves.
There is no one-stress-fits-all
This is the point worth carrying away from everything above. Every stress level in ESS, HALT and HASS is determined empirically, on your product, in your configuration. A profile that is correct for a ruggedized industrial controller will do nothing for a densely packed telecom board and may destroy a delicate instrument.
Step the stress up. Watch what fails. Analyze it, fix it, and step again. Then screen inside the limits you found — and keep watching, because the moment a process changes, the limits you measured are the only reference you have.
*Measured 4" above center of table, −65 °C to +100 °C.